The tradition & historical record
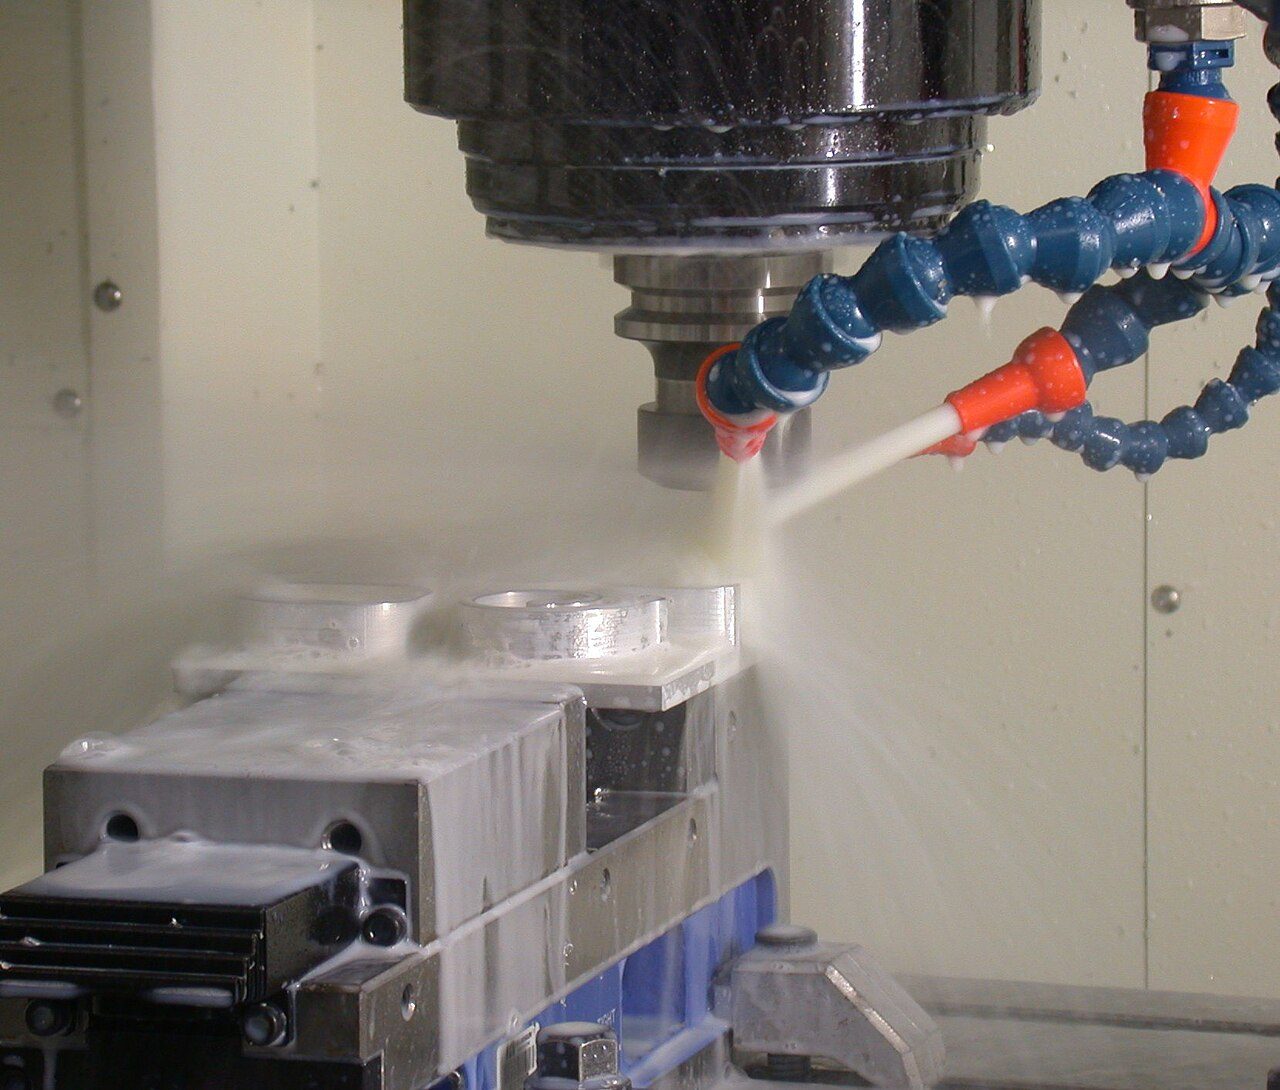
5 min read · 2 sourcesCutting fluid is a type of coolant and lubricant designed specifically for metalworking processes, such as machining and stamping. There are various kinds of cutting fluids, which include oils, oil–water emulsions, pastes, gels, aerosols (mists), air, and other gases. Cutting fluids are made from petroleum distillates, animal fats, plant oils, water and air, or other raw ingredients. Depending on context and on which type of cutting fluid is being considered, it may be referred to as cutting fluid, cutting oil, cutting compound, coolant, or lubricant. Most metalworking and machining processes can benefit from the use of cutting fluid, depending on workpiece material. Common exceptions to this are cast iron and most types of brass, which may be machined dry. The properties that are sought after in a good cutting fluid are the ability to: 1
Keep the workpiece at a stable temperature (critical when working to close tolerances). Very warm is acceptable, but extremely hot or alternating hot-and-cold are avoided. Maximize the life of the cutting tip by lubricating the working edge and reducing tip welding. Ensure safety for the people handling it (toxicity, bacteria, fungi) and for the environment upon disposal. Prevent rust on machine parts and cutters. 1
Cooling
Metal cutting generates heat due to friction and energy lost deforming the material. The surrounding air has low thermal conductivity (conducts heat poorly) meaning it is a poor coolant. Ambient air cooling is sometimes adequate for light cuts and low duty cycles typical of maintenance, repair and operations (MRO) or hobbyist work. Production work requires heavy cutting over long time periods and typically produces more heat than air cooling can remove. Rather than pausing production while the tool cools, using liquid coolant removes significantly more heat more rapidly, and can also speed cutting and reduce friction and tool wear. However, it is not just the tool which heats up but also the work surface. Excessive temperature in the tool or work surface can ruin the temper of both, soften either to the point of uselessness or failure, burn adjacent material, create unwanted thermal expansion or lead to unwanted chemical reactions such as oxidation. Regulating the heat created during machining processes is necessary to extend tool life, prevent the alteration of the workpiece's heat treatment, and prevent warping of the piece. The use of cutting fluids allows machinists to cut faster than they would be capable of if relying on surrounding air to cool the workpiece. Studies on alloyed structural steels used in power engineering have demonstrated that lubricating liquids may significantly modify chip formation mechanisms and the morphology of cutting products during turning operations. Further investigations have shown that technological modification of 38KhN3MFA rotor steel can alter its structural-phase state and affect chip morphology under variable machining conditions. 1
Lubrication
Besides cooling, cutting fluids also aid the cutting process by lubricating the interface between the tool's cutting edge and the chip. By preventing friction at this interface, some of the heat generation is prevented. This lubrication also helps prevent the chips from being welded onto the tool, which would interfere with subsequent cutting. 1
Rehbinder effect
The Rehbinder effect is the reduction in strength of a material when a surfactant, available in cutting fluids, is applied. Cutting fluid coats the cutting surface and reduces its surface energy, effectively weakening the material. This decreases the force required to make cuts, the wear on tools, and the time required for machining processes. The Rehbinder effect is complicated, relying on the chemical properties and structures of both the cutting fluid and working material, and is therefore difficult for machinists to factor into the planning of machining processes. Experienced machinists may utilize "rules of thumb" or trial and error methods if they consider the effect at all. 1
Extreme pressure additives
Extreme pressure additives in cutting fluids create a barrier between the cutting tool and working material. This barrier prevents contact between the two. If the cutting tool and working material were to make contact, particles from the working material could be welded to the cutting tool. These added particles would decrease the accuracy of the tool and its cuts, increase the friction in cutting, and lower the quality of the surface finish. 1
Delivery methods
There are several different delivery methods of cutting fluids that are used in machine cutting, this includes: 1
Dry Machining MQL Machining Cryogenic Machining Pressure or Jet Cooling Flooded Cooling Cryogenic MQL Machining Dry Machining doesn't use any lubrication during the machining process. Dry machining has fewer economic and ecological impacts than other delivery systems. It often causes temperature increases, which can affect tool life. Minimum Quantity Lubrication (MQL) Machining is a delivery system where a small amount of lubrication is used during machine cutting instead of using large amounts of fluid. MQL is regularly used due to its ability to extend tool life while remaining eco-friendly. Cryogenic Machining uses cryogenic liquids as coolant with a regulated pressure and volume. This pressure and volume increase the tool life of the machine while simultaneously improving the surface finish on the products. Cryogenic Machining is also considered to be a sustainable option due to its environmentally friendly nature. Pressure or Jet Cooling uses high-pressure water/liquid that sprays directly on the machine cutting surface. Flood cooling is widely used in machining and typically involves an oil-water mixture as the cutting fluid. For machining additively manufactured metals, biodegradable vegetable-based oils are often chosen by companies. The fluid will cover, flood, the cutting zone during machining. This method combines water's cooling ability with oils lubrication, but the flow rate must be regulated properly for effective temperature control and performance. Cryogenic MQL Machining is a combination of Cryogenic Machining and MQL Machining. 1
The text above is adapted from the Wikipedia article “Cutting fluid”, available under the Creative Commons Attribution-ShareAlike 4.0 licence. 1
cutting fluid is type of coolant and lubricant designed specifically for metalworking processes, such as machining and stamping, according to the structured record cited below. This entry was generated automatically from that record and has not yet been reviewed by a person familiar with the tradition. 2
The source record links this tradition to 12 external registers, which can be verified through the citation. 2